
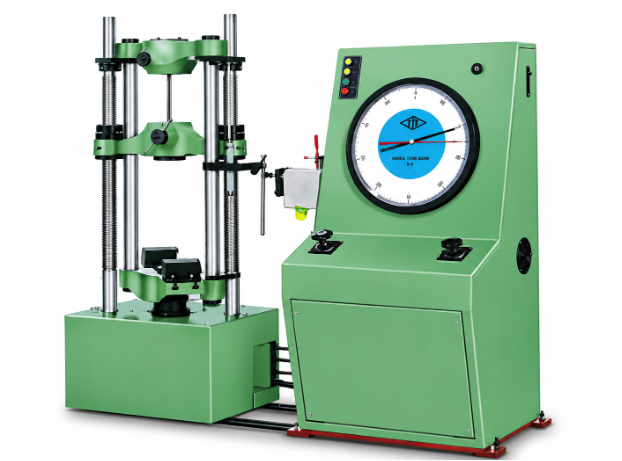
A universal testing machine (UTM) under a quality system carries a due date for its next force verification, and sooner or later someone asks how that date was chosen. An auditor asks why the cycle runs twelve months and not six. A customer disputing a result wants to know whether the machine was in tolerance on the day that specimen broke. Answering that takes the next certificate as well as the last one.
Most laboratories calibrate a universal testing machine’s force system at least once a year, and heavy use, tight tolerances or a regulated program often shorten that to six months. A move, a major repair, a new load cell, an overload or results that suddenly look wrong call for verification before the due date, however far off that date is. Where a customer specification, the laboratory’s quality system or an accreditation program sets the interval, that document has the final word.
The right figure for a particular machine depends on how much rides on its results and on its found history, the errors recorded before any adjustment.
Force verification sits at the center of the schedule, and it works the same way on electromechanical and servo-hydraulic testing machines. It examines the measuring chain from load cell to readout, whether ballscrews or a hydraulic actuator supply the load. Strain measurement, displacement and load train alignment lie outside that chain, and each is usually verified as a separate item.
When A Year Between Verifications Is Too Long
Whatever interval a laboratory chooses, the due date is a hard limit. Tensile test methods such as ASTM E8/E8M assume the machine has a current force verification, and yield and tensile strengths reported after it lapses are difficult to defend in an audit.
A twelve-month calibration interval is the usual starting point. It lines up with internal audits and customer reviews, and it turns calibration downtime into planned service instead of an urgent fix.
A machine that spends much of its day near capacity is more likely to drift or wear, in the force-measuring system and in the mechanical stack. That drift surfaces in the as found results over successive visits. Heavy daily use and tight tolerances often drive a six-month interval for that reason. Plants that run a machine daily tend to keep the interval conservative and watch the drift trend.
Risk pulls the same way. Where one report can hold a shipment, reject a lot or support a certification decision, the calibration program usually needs shorter intervals, more detailed records and a stronger traceability chain. High-volume and regulated programs often settle on six months, as does critical aerospace work. In aerospace and defense, machines that support production release testing tend to get shorter intervals or tighter internal rules.
The machine’s own record settles the rest. As found results that stay comfortably inside tolerance visit after visit support the current interval. Results that creep toward the limit, or an outright failure, are the signal to shorten it.
Where a governing document sets the interval, that figure stands. Before writing it into a procedure, the laboratory should confirm which edition of ASTM E4 or ISO 7500-1 the document cites, since revisions can change verification details.
A six-month cycle costs one extra service visit a year. A failed as found result at the end of a twelve-month cycle can put up to a year of reported results under review.
Five Events That Call For Verification Before The Due Date
A due date assumes the machine stays as the technician left it. Most laboratories treat the following events as triggers for verification even when the next date is months away:
- A move or reinstallation, including a new foundation or a change in power conditions.
- A rebuild or major repair, including any controller work that touches the measurement chain.
- A new load cell or force transducer.
- An overload, or any suspicion of mechanical damage.
- Results that look wrong, such as an abnormal value, a correlation check that fails, or scatter that suddenly widens.
Each one changes the machine the current certificate describes, or suggests that it has changed. Until a fresh verification, results reported after the event rest on evidence gathered before it.
Strain Measurement Needs Its Own Calibration And The Right Class
A current force certificate covers the force reading and nothing beyond it. Once a report includes offset yield, elongation or modulus, the extensometer becomes a primary measuring instrument, calibrated and classified under ASTM E83 or ISO 9513.
The class matters as much as the date. It decides which properties the extensometer can report, and modulus and proof strength need the tightest classes. An extensometer classed too coarsely for modulus can invalidate the result even when its calibration is current.
Most laboratories put the extensometers on the same twelve-month cycle as the force system. Calibrating them during the same visit verifies force and strain together and gives both records one date.
Displacement and speed come into scope when the test record reports crosshead displacement or the method relies on machine speed. The displacement device or the speed control may then need its own verification.
A laboratory that schedules force alone can hold a current certificate and still report a modulus it cannot defend.
Off-Axis Loading Can Hide Behind A Passing Force Certificate
A frame can pass force verification with margin to spare and still pull its specimens off axis. Force verification measures the accuracy of the load reading. It says nothing about the path that load takes through the specimen.
Bending adds stress on one side of the specimen and removes it from the other, which biases yield, tensile and fatigue results and can cause early or off-axis failures. A familiar symptom is stiff or brittle material breaking outside the gauge section at loads that seem too low. Scatters that get blamed on the material can start in the load train.
ASTM E1012 measures the bending with a strain-gauged alignment specimen installed in the grips or fixtures used for production testing. The technician records bending strain against axial strain at set load levels and compares the percent bending with the class or limit that the applicable test method requires. If it exceeds that limit, the grips, adapters or alignment fixture need adjusting before the check runs again.
Because the check runs with the production grips and fixtures, its result describes that particular load train, and mismatched adapters are a known source of off-axis loading. A laboratory’s budget can carry the alignment check as a yearly item alongside force verification. Extra checks make sense before critical runs, after the frame has moved, and when two machines disagree for no visible reason.
Measuring misalignment does not correct it. Where the bending is too high, a load-train alignment device mounted between the crosshead and the grips allows coarse positioning and then fine adjustment against a built-in coaxiality indicator. It can be retrofitted to a frame already in service, and the corrected alignment can be checked against ASTM E1012 and documented for the audit file.
Aerospace laboratories audited under Nadcap must show that their tensile and fatigue frames are aligned within allowed tolerances, often with strain-gauged specimens per ASTM E1012. Alignment left uncontrolled can become an audit nonconformance, and accreditation then waits until it is resolved.
What The As Found Data Says About Results Already Issued
When a certificate comes back, the first figures to read are the ones recorded before the technician touched anything. Those found results describe the machine during the testing since the last visit. The left results, taken after any adjustment or service, describe it from the visit onward.
The pass or fail line says less than the table beneath it, which should list applied and indicated force at each verification point with the error as a percentage. That table shows how close each point came to the limit, commonly 1 percent of reading under ASTM E4. ISO 7500-1 assigns a class instead, from class 0.5 (a relative error of 0.5 percent) to class 3 (3 percent). Tensile test methods name the class they require, ISO 6892-1 for room-temperature tensile testing of metals among them.
Under ASTM E4, the lowest force at which the machine met the tolerance sets the bottom of the verified range. Results produced below it fall outside what the verification supports. For contract testing, the range on the certificate should cover the loads actually tested.
The rest of the certificate shows whether those numbers can be trusted. It should state:
- The standard and its edition year.
- The machine’s serial number and asset ID.
- The modes covered (tension, compression or both).
- The reference instrument and its own calibration, to ASTM E74 for ASTM E4 work or to ISO 376 under ISO 7500-1.
- The measurement uncertainty and the conditions during the visit.
- As found and as left results if anything was adjusted, and the next due date.
The difficult case is an as found result outside tolerance. It means results issued since the previous verification may have come from a machine that was not meeting its requirements. The internal review that follows sets the tests run in that period, and the forces they used, against the as found errors. A corrective action record closes it out, and auditors usually look for one when the machine serves production testing in that period.
Superseded certificates stay in the file rather than being deleted. When a result is disputed, the first question is often whether the machine was in tolerance on the day of the test. The certificates on either side of that day hold the answer.
Setting a new certificate’s as found errors beside the as left errors on the previous one shows how far the machine moved during the interval. That gap is the evidence for keeping the interval or shortening it.
Calibration Questions That Come Up Between Audits
Seven questions tend to come up when a calibration schedule is set or challenged.
- What Does As Found And As Left Mean On A Calibration Certificate?
As found data shows how the machine performed before the technician changed anything, and as left data shows its performance after adjustment or service. An out-of-tolerance as found result can therefore trigger a review of testing already reported.
- Is Annual Calibration Enough For A Heavily Used Testing Machine?
Not always. Heavy daily use and tight tolerances often drive a six-month interval, because a machine that runs near capacity is more likely to drift or wear. As found, results that move toward the limit between annual visits are the sign that a year is too long.
- Does A UTM Need Recalibration After A Move?
Yes. Most laboratories treat a relocation or reinstallation as a trigger for verification, even when the due date is months away. A basic check of alignment and measurement accuracy after the move helps confirm the setup in its new location.
- Does Replacing A Load Cell Require A New Calibration?
Yes, whatever the due date says. A new load cell or force transducer changes the measuring chain that the previous verification covered, so the existing certificate no longer describes the machine.
- Can Results Be Reported Below The Verified Force Range?
Not on the strength of that verification. Under ASTM E4 the verified range starts at the lowest force at which the machine met the tolerance, and the certificate supports nothing beneath it. Where low-force work matters, the verification has to reach down to the forces actually used.
- Is ISO 17025 Calibration The Same As ASTM E4 Verification?
No. ASTM E4 and ISO 7500-1 define what a force verification contains, while ISO/IEC 17025 governs how a competent laboratory performs and documents that work, including traceability and measurement uncertainty. The accreditation belongs to the calibration provider, so its scope should cover force, extensometers or alignment at the ranges in use.
- What Should Be Ready Before The Calibration Technician Arrives?
The production grips and fixtures should be installed, with worn jaw faces replaced, and the electronics warmed up. Alignment specimens go into the normal setup so the check reflects real testing. The previous certificate should be on hand for comparison with the new as found data.